

Profiling plantLinia CZS
Zeman




Dados básicos
- Designação da máquina:
- Profiling plant
- Fabricante:
- Linia CZS
- Modelo:
- Zeman
- Ano de fabrico:
- 2010
- Condição:
- quase novo (usado)
- Funcionalidade:
- totalmente funcional
Preço e localização
- Localização:
- Mariusza Bojemskiego 9, 42-202 Częstochowa, Polska
Detalhes da oferta
- ID do anúncio:
- A21299532
- Atualização:
- por último em 22.10.2026
Descrição
ZEMAN CZS LINE SPECIFICATIONS.
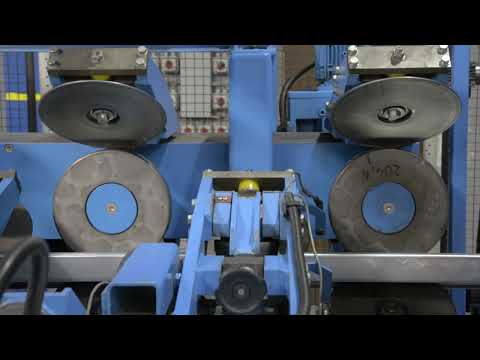
ZEMAN's flagship product, the fully automated "PURLIN" line, is used to produce open, cold-formed sections such as C, Z, and SIGMA, in various widths and shapes, thanks to fully automatic adjustment of the profiling rollers. Coils up to 750 mm wide and 1.25 mm to 3 mm thick sheet metal in grade S-390 and lower can be used as raw material. The machine is designed to produce components up to 15 m long. The width of the specially hardened profiling rollers is infinitely adjustable, using only dedicated software. A fully integrated "flying punching" device creates all types of mounting holes, and the entire process is continuous, meaning the material does not stop for individual operations such as punching holes or cross-cutting. To maintain production efficiency, the line speed is dynamically optimized. The machine decelerates and accelerates automatically without operator intervention.
A coil uncoiler with a maximum working load of 15 tons is mounted on a mobile trolley, enabling precise centering of the material strip before feeding it into the straightener.
The straightener, along with a crescent straightening system, allows for straightening the material, ensuring the required sheet flatness and reducing the crescent on the feed belt.
2. Punching Section
This section contains 5 double, "flying" punching portals, which can be equipped with 20 small (up to 40 mm) or 10 large (up to 100 mm) tools (punches and dies) for punching mounting holes.
A combination of these tools can also be used.
3. Pre-cutting Shear
A "flying" shear used to make preliminary holes for the cutting shear. This process is designed to maintain material continuity, resulting in a more precise profile shape, especially at its beginning and end. This is an adaptive guillotine that adjusts the width of the hole being cut to the width of the sheet metal strip.
4. Guide Carriage/SIGMA Modules
The guide carriage is used to center the sheet metal strip before entering the profiler. It is interchangeable
with the module for producing Sigma-shaped profiles. To produce S+ profiles,
the guide table should be removed and two Sigma modules inserted. These modules position
fully automatically and independently, left and right.
6. Rotary Cut-Off Guillotine.
Djdpfx Ajymampsqrewd
The rotary cut-off guillotine with hook knives is used to finally cut the profile from the material strip
using the holes made by the pre-cutting guillotine. This is a "flying" guillotine,
so the sheet metal does not stop during the cutting process. Depending on the profile being produced, a properly oriented cutting cassette should be attached.
7. Receiving Table
The receiving table is used to automatically discharge the completed profiles from the roller conveyor. The elements are then manually arranged into a package. The design allows for easy bundling of the package. The table is designed to accept 15-meter profiles and allows for access by a forklift or overhead crane to collect the package of profiles.
Fornecedor
Registrado desde: 2006
176 Anúncios online

Enviar pedido
Telefone & Fax


 Hagen
DMGDMC 1035 V


 Moldávia
Mechanika MaszymLRV


 Vilalba
DemaqEvo 4.0


 Weilerswist
TEMAREDCar Flat 3518 für PKW bis 1.438 kg - Kippbar


 Alemanha
GildemeisterCTX 200E


 Beograd
GaspariniSlitter


 Düsseldorf
DECKEL MAHODMF 250 Linear


 Winkelhaid
KeaserSM12


 Staufenberg
DURMAAD-S 30175

 Fevziçakmak
TFON MACHINE CO.Leveling Machine | TF-L 9016

Selo de confiança Machineseeker
O que é o selo de confiança?
Machineseeker certifica revendedores selecionados com o selo de confiança Machineseeker. Antes da atribuição, é realizada uma inspeção normalizada e abrangente por funcionários experientes da Machineseeker.
O que verificamos?

Verificação do
alvará comercial ou do extrato do registo comercial
Verificação do
endereço postal do vendedor
Validação da
ligação bancária
Verificação da
acessibilidade telefónica
do número principal
A informação comercial
não deve apresentar características negativas
Reclamações de compradores
podem levar à retirada do seloO que isto significa para si enquanto comprador?
Com o selo de confiança Machineseeker, você pode, como comprador, identificar vendedores confiáveis sem necessidade de avaliação própria, que provavelmente realizam negócios honestos e íntegros.
Naturalmente, durante o processo de compra podem ainda surgir divergências de opinião. A Machineseeker não se responsabiliza por infrações legais cometidas por compradores ou vendedores ativos na plataforma Machineseeker.